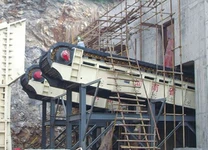
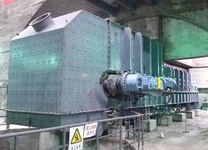
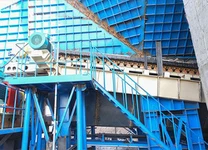
One copper mine of our company is an open-pit copper mine, with two beneficiation production systems, all of which use cement apron feeder to feed ore to belt conveyor. With the development of the mine and the improvement of production capacity, the service life of the cement apron feeder will gradually decline, and the replacement and maintenance of the cement apron feeder is the main maintenance workload, so it is particularly important to extend the service life of the cement apron feeder.
Specification of cement apron feeder 1200mm×6048mm, width of chain plate 1200mm, distance from sprocket shaft line to tensioning shaft line 6048mm, feeding speed range (0.0640.1)m/s(frequency conversion speed regulation), Production capacity (200-350)/ small h, feeding particle size ≤300mm, material density 1960k/m3, motor model YP2-180m-4,18.5kW, reducer model number M5RHT60, speed ratio 436.87.

The cement apron feeder should use wear-resistant steel plates on both sides of the inner silo, and the service life of the plates is short, about 6 months. The root of the mounting bolt of the guard plate is seriously worn, and the guard plate has the risk of falling off, causing a safety hazard for the next process. Replacement of guard plate is the main cause of heavy plate to the mining machine shutdown maintenance, each replacement of guard plate time consuming power, seriously restricts the work efficiency of heavy plate mining machine. According to the operation analysis, the wear surface of the protection plate is smooth and uneven, and the wear at the bottom is more serious than the upper part. It is mainly due to the relative movement of ore and the guard plate, resulting in sliding friction and extrusion pressure, resulting in the wear of the guard plate: Because the ore falls from the ore pile to the chain plate of the heavy plate feeder, the faster the speed of the bottom ore movement, the greater the extrusion pressure, according to the principle of action and reaction force, the bottom of the guard plate by the ore extrusion pressure and friction force is greater, so the bottom of the guard plate wear more serious.
(1) Add bolt protection devices. A 20mm thick round boss is designed at each bolt hole position to protect the bolt. (2) Add "ore storage tank" (Figure 1). According to the wear track of the material ore, add a section of wear-resistant bars with length, width and height of 470mmx30mm×40mm to the upper part of the protection plate, and add three sections of wear-resistant bars with length, width and height of 1075mmx30mm× 40mm, 400mm×30mm×40mm and 250mm×30mm×40mm to the bottom respectively. When the heavy plate feeding machine is in operation, the "ore storage tank" has a full tank of powder ore and small ores due to friction and extrusion, the part of the ore and the guard plate is relatively static, subtly the ore and the guard plate extrusion, friction into the ore and the ore and the ore, the formation of the protective layer of the guard plate, greatly prolonging the service life of the guard plate.
4. Optimize the service life comparison of cement apron feeder plate before and after Cement apron feeder
Through the structural optimization design of the cement apron feeder on both sides of the mine silo, the problems of uneven wear and serious wear of the cement apron feeder have been completely solved, and the service life of the optimized shield has been extended from 6 months to 24 months.
The implementation of the program has achieved good results and achieved the expected goal. The structure of the shield plate was optimized, which solved the problem of short service life of the shield plate, reduced the frequency of cement apron feeder downtime and maintenance, reduced the labor pressure of maintenance personnel, and improved the operation efficiency of the equipment and the stability of the production system.